Quick wins for a faster PC:
Repair Windows errors before they cause bigger problemsFix Now →Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →ThatPainter is reader-supported. When you buy through links on our site, we may earn an affiliate commission. Learn More
An Ender 3 normally feeds heated plastic filament through a hot end. This adaptation replaces that system with a pressurized clay feed, an auger, and a ceramic-printing nozzle—turning a familiar FDM motion platform into an experimental clay printer.
What the project changes
Featured in Hackaday’s August 22, 2023 report, maker davidsfeir adapted an earlier clay-extrusion approach for compatibility with an Ender 3. The printer’s frame and motion system position the tool, but the tool itself is fundamentally different from a filament extruder.
Clay is delivered through a clear tube from a lightly pressurized reservoir. An auger, or screw, then moves and homogenizes the clay before forcing it through a nozzle. An opening near the upper, motor-side portion of the extruder provides a route for trapped air to escape instead of sending it through the printed bead.
Windows Errors? Fix Them Before They Spread
Repair common Windows errors and clear accumulated junk for a smoother, more stable PC - no reinstall needed.Free scan · no reinstallOutdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware match#1 Best Overall

- 11. Product highlights: No need to change the 3D printer firmware. Regular 3D printer+clay push rod professional version kit equals direct writing clay 3D printer
- 12. Working principle: Short range screw extruder+ remote pushing rod(Motor-drive Rod) feeding system
- 13. Supporting materials: Most soft flowing materials such as clay, colloids, and semi fluid
- 14. Nozzles: 12 stainless steel nozzles (short version) and 12 plastic nozzles (long version), each 1.5mm 2.0mm 2.4mm 3.0mm
- 15. Suitable model: Most FDM principle 3D printers on the market
- A pressurized clay reservoir and feed tube
- An auger-driven extrusion mechanism
- A clay-compatible nozzle
- An air-escape path near the top of the extruder
- A custom mount for an Ender 3-style printer
Why a normal filament extruder cannot print clay
FDM hardware is designed around a solid, flexible filament. A drive gear grips the filament, a heater melts it, and a nozzle deposits the comparatively predictable flow of polymer. Clay is a dense, wet paste: it cannot be spooled, melted, or reliably pushed by a filament gear.
That changes the engineering problem. The material must be stored somewhere, transported through a hose, and pushed through the nozzle under controlled pressure. The auger is not simply a substitute for a hot end. It helps move the paste, compress it, and maintain a more consistent flow while the printer supplies the X, Y, and Z motion.
The Hackaday report does not specify universal pressure, flow-rate, nozzle, speed, or layer-height settings. Those variables depend on the clay body, tube length, auger geometry, nozzle, and printer conversion.
The important idea: giving trapped air somewhere to go
Air is one of the main enemies of paste extrusion. Bubbles can produce voids, weak sections, intermittent flow, sudden spurts, and poor layer starts. A simple syringe or sealed chamber may carry those bubbles directly toward the nozzle.
The Tool Desk
Outbyte PC Repair FREEClear out junk files and repair common Windows errorsFree Scan →Outbyte Driver Updater FREEFix the driver behind crashes, sound loss and screen glitchesFind Drivers →The featured extruder instead leaves a gap near the upper part of the mechanism. As the auger moves clay downward, air can escape through that opening. This should be understood as an air-management feature, not proof that the clay is completely de-aired. The design draws on earlier work associated with Jonathan Keep and Piotr Waśniowski’s de-airing clay extruder.
Rank #2

- Foldable Ceramic 3D Printer: Building Size: 250*250*260mm. Loosen the bottom retainer, pull up the frame, and tighten the 4 screws to complete the installation.
- Adapted Materials: Clay, Ceramics Slurry, Red Porcelain and various liquid flowing materials. A household microwave can serve as a kiln, can be glazed in 35 minutes
- Major Equip: Dual axis metal guide rail, runs smoothly and stably, easy maintenance. TMC2209, 32 Bit Silent Main board, LDM Extruder for clay 3D printing, resume printing after power outage
- Fast Printing: Replaceable, adjustable synchronous feeding system, faster than the previous 3d printer series with a maximum print speed of 40mm/s.
- No need air compressor: Developed electric putter instead of compressed air to make sure outstanding printing quality and stability for prints.
Clay consistency determines whether the print survives
Printable clay has to balance several conflicting requirements. It must be soft enough to travel through the tube and nozzle, cohesive enough to form a continuous bead, and stiff enough to support the layers above it. It also needs to be homogeneous and free of large particles that could block the nozzle.
Too-wet clay may slump or collapse. Too-stiff clay may require excessive pressure, clog the system, or overload the auger. Dry lumps and coarse particles can create the same problems even when the overall mixture seems workable. WASP’s clay-printing guidance likewise emphasizes preparing a homogeneous clay mass without air bubbles.
There is no single recipe that works for every conversion. Clay body, particle size, nozzle diameter, pressure, tube length, layer height, and print speed all affect the result.
Printing is only the first ceramic step
The object leaving the nozzle is wet, unfired clay—not a finished piece of pottery. A typical workflow is:
- Prepare clay at a consistent, workable moisture level.
- Remove or minimize trapped air and load the feed system.
- Print the form with the clay extruder.
- Dry it slowly and evenly to reduce cracking and distortion.
- Bisque-fire the dry greenware.
- Apply glaze if desired.
- Fire it again according to the clay and glaze manufacturer’s guidance.
Drying and firing schedules are material-specific. The Hackaday article does not provide a schedule, shrinkage percentage, or kiln temperature for the featured work. Jonathan Keep’s guide to clay 3D printing provides broader context on clay preparation, printer conversion, file preparation, and post-print considerations.
Rank #3

- 【99% Pre-Installed and Print right out of the box】Liquid deposition Molding Ceramic 3D Printer,Building Size: 250*250*260mm;Materials: Clay, Ceramics Slurry, Red Porcelain and various liquid flowing materials.Contain 2 packs of clay for you to print happily.
- 【FOLDING STYLE 】Newly Designed Screw Feeding Device,and Replaceable Adjustable Synchronous Feeding System.
- 【NO NEED AIR COMPRESSOR】We developed electric putter instead of compressed air to guarantee outstanding printing quality and stability for prints. More easy to use for beginner.
- Rapid prototyping, high-speed printing-The maximum printing speed can reach 40mm/s, and the layer thickness can be set to 0.3-3mm.
- Dual axis metal guide rail, smooth and stable running, strong and durable
What an Ender 3 conversion does—and does not—promise
Using an Ender 3 matters because it reuses a widely available motion platform instead of requiring a purpose-built ceramic printer. For a maker who already owns one, that can make experimentation more accessible.
However, “Ender 3-compatible” is not the same as “a drop-in upgrade for every Ender 3.” Models and derivatives differ in carriage geometry, electronics, firmware, and available mounting space. A conversion may require a custom bracket, a different nozzle height, altered wiring, and slicer adjustments. Wet clay can also contaminate belts, rails, bearings, fans, and electronics, so the conversion may be better treated as a dedicated experimental machine rather than a temporary accessory.
Recommended Free Tools
What you would still need to reproduce it
The source establishes the overall concept, but it is not a complete build manual. It does not publish a complete bill of materials, dimensions, CAD files in the article body, pressure values, nozzle specification, clay formulation, firmware changes, slicer profile, assembly sequence, cleaning procedure, or expected cost.
A practical reproduction would therefore require more than printing a mount. You would need to resolve:
- How the reservoir is pressurized and safely connected to the feed tube
- How the auger is coupled to its motor
- How the upper air escape is sealed against clay leakage while remaining effective
- Which nozzle and clay body suit the desired bead size
- How extrusion starts and stops without pressure lag or blobs
- How the entire material path can be disassembled and cleaned
- How the printer is protected from wet clay
Do not increase pressure indefinitely when extrusion fails. Excess pressure can cause leaks, tube separation, sudden material release, or mechanical damage.
Rank #4

- [Ceramic Material Compatibility] Specialized for clay paste and pellet materials, enabling smooth extrusion for DIY ceramic 3D printing projects with consistent results.
- [Direct Extrusion Design] Direct extruder structure delivers strong pushing force, reducing material blockages and ensuring stable feeding for precise ceramic prints.
- [Complete Assembly Kit] Includes all necessary components for printhead assembly, eliminating the need for separate purchases and simplifying DIY setup.
- [Stepper Motor Integration] Works seamlessly with compatible stepper motors, providing accurate speed control to match ceramic material extrusion requirements.
- [Easy DIY Installation] Pre matched parts and simple assembly process allow enthusiasts to upgrade or build ceramic 3D printer printheads without complex tools.
Common failure modes
Intermittent extrusion
Check for inconsistent clay, dried residue, trapped air, an unstable pressure supply, poor auger engagement, or particles too large for the nozzle. Cleaning and preparing the clay are usually more useful than simply applying more pressure.
Flow continues after a move
Paste systems have pressure lag and flow inertia. Lower pressure, a slower feed rate, pressure-relief behavior, retraction, and travel-path changes may help, but the correct settings are specific to the extruder and are not supplied by the original report.
Layers collapse
Clay may be too wet, the layer height or bead width may be too large, the printer may be moving too quickly, or the geometry may lack support. A stiffer body, smaller layers, slower motion, pauses between layers, or redesigned overhangs can improve stability.
The fired piece cracks
Cracking can result from uneven drying, thick walls, trapped moisture, uneven wall thickness, an unsuitable firing schedule, or differential shrinkage between layers. Dry small test pieces first and follow the instructions for the specific clay body and glaze.
Independent reader supportYour contribution helps us test, update, and keep practical guides available for everyone.DIY conversion versus a dedicated clay printer
A DIY Ender 3 conversion suits makers who already own the printer and want to explore paste extrusion, custom mechanisms, and ceramic form-making. Its advantages are reuse, experimentation, and potentially lower hardware cost. Its disadvantages are incomplete documentation, model-specific compatibility, cleanup, contamination risk, and the need to solve the clay, pressure, and software workflow yourself.
Crashes, No Sound, or Screen Glitches?
Random freezes, missing sound and display glitches usually trace back to one bad driver. Find and replace yours safely.Free scan · under a minutePC Slower Than It Used to Be?
A free scan shows the junk files, broken settings and background clutter dragging Windows down - then fixes them in one click.Free scan · Windows 10 & 11Best Value
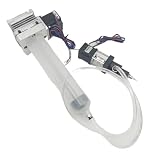
- Model Compatibility: Designed for Funssor Clay Paste Screw Extruder System assemblies in DIY ceramic printer kits.
- Functional Purpose: Replaces the worm gear pusher motor to restore extrusion functionality.
- Component Type: Worm gear pusher motor intended as a direct functional replacement part.
- Application Scope: Used specifically in clay paste extrusion systems for DIY ceramic printer assembly.
- Installation Context: Fits into existing Funssor Clay Paste Screw Extruder System configurations without modification.
A dedicated machine reduces some of that improvisation but does not eliminate the ceramic workflow. As a current commercial reference, WASP lists the Delta WASP 2040 Clay at €3,300 on its product page as observed in the supplied research. The listed machine has a nominal build volume of 200 mm in diameter by 400 mm high, standard nozzle options from 1.5 mm to 3 mm, and a stated minimum compressed-air requirement of 8 bar and 25 L/min. Prices and specifications can change, and the machine still requires clay preparation, a compressor, controlled drying, and kiln access.
A syringe or piston extruder is another possible architecture. It may be simpler to understand, but its capacity and pressure behavior can make continuous extrusion more difficult. An auger/de-airing system is mechanically more involved, yet it is better aligned with continuous clay transport and air management. Neither approach is automatically successful without matching the clay and toolpath to the mechanism.
Safety and cleanup
Keep wet clay away from exposed electronics, fans, motors, and moving bearings. Inspect the tube, fittings, nozzle, and auger for leaks before applying pressure. Release pressure before disconnecting any part of the feed system. Clean the material path while the clay is still wet; dried clay is much harder to remove and may damage components during reassembly.
For firing, use a kiln and ventilation appropriate to the clay and glaze being used. Never assume that a printed form is safe to handle, heat, or use simply because it has come off the printer.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
Bottom line
This project makes clay printing more approachable by adapting a specialist paste-extrusion idea to an Ender 3 motion system. Its key innovations are the pressurized feed, auger-driven material transport, and upper air-escape path. But it is an experimental conversion, not a fully documented consumer upgrade: successful results still depend on clay preparation, pressure control, custom mechanical work, cleaning, careful drying, and ceramic firing.
Quick Recap

Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.